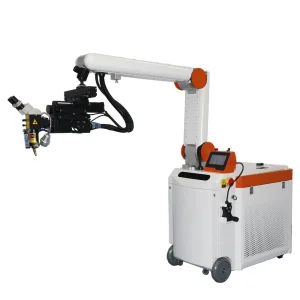
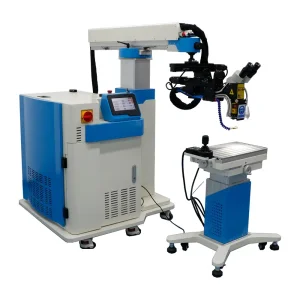
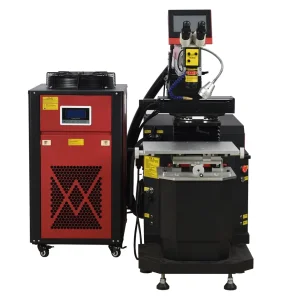
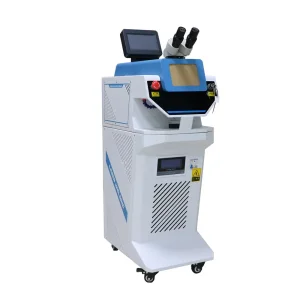
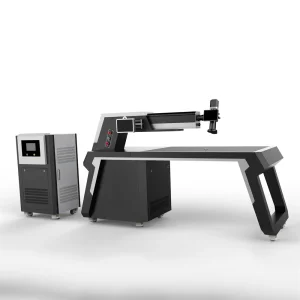
Engineered for immediate toolroom deployment across Pirkanmaa machine shops, offering low-heat input repair for P20, H13, Stavax, and tool steels without pre-heating.
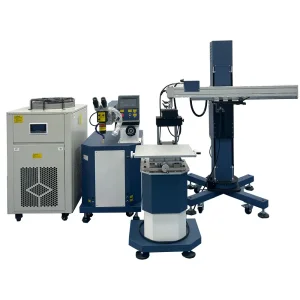
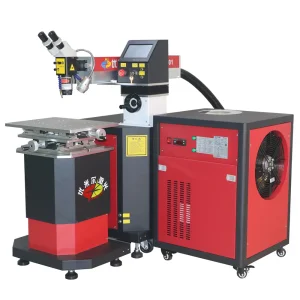
As the industrial heartland of Finland and the core of the Pirkanmaa economic corridor, Tampere houses a concentrated cluster of world-class mechanical engineering, automated mobile machinery (Sandvik, Kalmar, Cargotec, Valmet ecosystems), and high-specification precision tooling workshops.
For plastic injection molders in Pirkanmaa producing medical disposables, technical telecommunications components, and polymer consumer casings, mold wear is an existential overhead. Traditional TIG deposition introduces excessive heat-affected zones (HAZ), resulting in thermal fatigue, dimensional warping, metallurgical annealing of base steels (such as 1.2343, 1.2344, 1.2083, and Ramax), and days of secondary CNC EDM spark erosion or manual stoning.
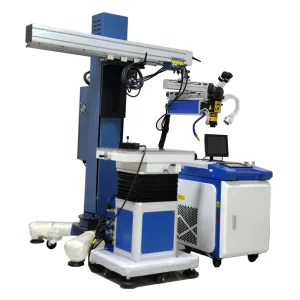
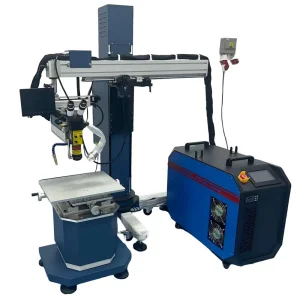
Youmir Laser’s Mold Laser Welding Series addresses Tampere’s exact requirement: providing sub-micron control, micro-pulse laser cladding without pre-heating, and localized in situ repair capabilities that keep heavy 10-tonne injection blocks on the machine platen while restoring parting lines, sharp knife-edges, pinholes, and gate cracks within fractions of a millimeter.
High capital costs, compressed prototype-to-production windows, and supply chain vulnerability for specialized alloy billets make mold repair far superior to mold remake.
Unlike conventional arc deposition which melts wide sections of surrounding matrix, pulsed fiber and QCW laser welding create a localized micro-fusion pool. The dilution rate remains below 5%, eliminating crystalline embrittlement, stress cracking, and sink marks on polished mold surfaces.
A medium-scale automotive interior tooling assembly costs upwards of €80,000 to €250,000. Replacing worn shut-offs via laser deposition costs under 2% of tool replacement value, returning capital assets to active production in under 8 hours with zero metallurgical penalty.
Finnish manufacturing operates under strict European Union corporate sustainability directives (CSRD). Revitalizing production molds through precision additive repair avoids scrap steel waste and drastically lowers total life cycle embodied carbon emissions.
| Evaluation Parameter | Youmir Fiber Mold Welder | Youmir QCW Pulsed Series | Traditional TIG / Micro-TIG | Secondary Re-machining / Remake |
|---|---|---|---|---|
| Heat Affected Zone (HAZ) | 0.03 - 0.08 mm | < 0.03 mm (Cold Weld Effect) | 1.20 - 3.50 mm (Severe) | N/A |
| Micro-Hardness Retention | 100% matched to filler alloy | 100% (No base metal softening) | Anneals base metal (-20% to -40% HRC) | Complete re-hardening required |
| Spot Diameter Precision | 0.20 mm - 1.80 mm adjustable | 0.10 mm - 1.50 mm micro-fine | 1.5 mm minimum electrode arc | Sub-micron CNC milling |
| Tooling Preheating Need | None required for standard tool steels | None required (Direct cold strike) | Mandatory 250°C - 450°C preheat | Extensive thermal cycles |
| Direct In Situ Machine Repair | Yes (Boom / Cantilever Series) | Yes (Mobile Articulated Arm) | Extremely difficult / Fire risk | Impossible (Tool must be unmounted) |
| Estimated Toolroom ROI | 3 to 5 Months | 4 to 6 Months | High downstream benching cost | Negative capital depreciation |
Industrial machinery entering Finnish enterprises must meet the highest safety, electrical, and ergonomic standards enforced by Tukes (Finnish Safety and Chemicals Agency).
Youmir Laser machines delivered to Tampere and greater Finland are fully compliant with EU Directives and CE specifications:
Our international engineering division provides English-speaking technical diagnostics 24/7. Tampere toolmakers can send high-resolution macro photos or CAD scans of cavity defects, and our metallurgical technicians will calculate the optimal waveform, pulse frequency, and wire alloy match within 2 hours.
From injection molding shopfloors in Hervanta to heavy forestry machinery die casting facilities across Pirkanmaa, Youmir Laser machines provide precision repairs across multiple industries.
Rebuilding worn parting lines, sharp knife-edges, pinholes, and corroded cooling channels on high-cavity tools (medical syringes, electronics enclosures, automotive ducting). Works flawlessly on pre-hardened 1.2738, 1.2083, and mirror-polished Stavax ESR surfaces without micro-porosity.
Repairing severe thermal fatigue cracking (heat checking), erosion wear, and washouts in H11/H13 tooling used for automotive transmission housings, forestry equipment hydraulic valve blocks, and electric powertrain castings.
Edge buildup and chipped corner reclamation on D2, 1.2379, and cemented carbide punches without drawing the temper of surrounding cutting edges. Significantly extends the operational lifecycle between comprehensive tool overhauls.
Nokia and Pirkanmaa have deep industrial roots in elastomeric and heavy vehicle tire engineering. Our flexible cantilever laser welders restore fine sipping blade inserts, vent channels, and sidewall engraving plates on massive steel and forged aluminum segmented tire molds.
Hardfacing wear-prone surfaces on hydraulic hammers, drill chucks, and wear guides with carbide-bearing metal cored wires. Laser deposition yields higher bond strength and toughness than plasma transferred arc (PTA) or spray coating.
Accommodate late engineering change orders (ECOs) directly on hardened injection molds without stripping the tool. Add boss features, shift parting line ribs, or seal off unwanted pin holes cleanly and accurately.
Youmir Laser is actively investing in AI-driven optical tracking, hybrid additive manufacturing (Directed Energy Deposition ± Subtractive 5-axis Milling), and synchronized multi-axis robotic boom architectures.
For Tampere’s Industry 4.0 front-runners, the path forward shifts from manual stereomicroscope alignment to automated visual defect mapping. Our R&D pipeline integrates real-time structured light 3D metrology scanning heads onto our articulated cantilever welders. The system autonomously identifies chipped cavity profiles, references the original CAD model, calculates dynamic toolpaths, and deposits precise filler wire layers with adaptive closed-loop energy modulation.
This automated feedback loop ensures 100% metallurgical repeatability, removes operator variance, and optimizes finish allowances to under 0.1 mm, drastically slashing down-stream CNC EDM spark erosion and high-speed milling cycles.
Up to 300Hz dynamic oscillatory patterns eliminating keyhole gas pores and improving sidewall wetting on deep mold rib cavities.
Dual-camera optical seam tracking that compensates for operator hand tremors and adjusts laser pulse output dynamically.
Autonomous mobile industrial robots (AMRs) mounting QCW laser end-effectors for lights-out repair of die casting machinery.
Detailed metallurgical, operational, and commercial insights directly answered by Youmir Laser application engineering specialists.
Contact Shenzhen Youmir Laser Technology Co., Ltd. today for personalized parameter calculations, sample testing on your mold alloys, and an official FOB/CIF Tampere quotation.
Full lineup serving Pirkanmaa toolmaking, precision jewelry crafting, and industrial fabrication workshops.